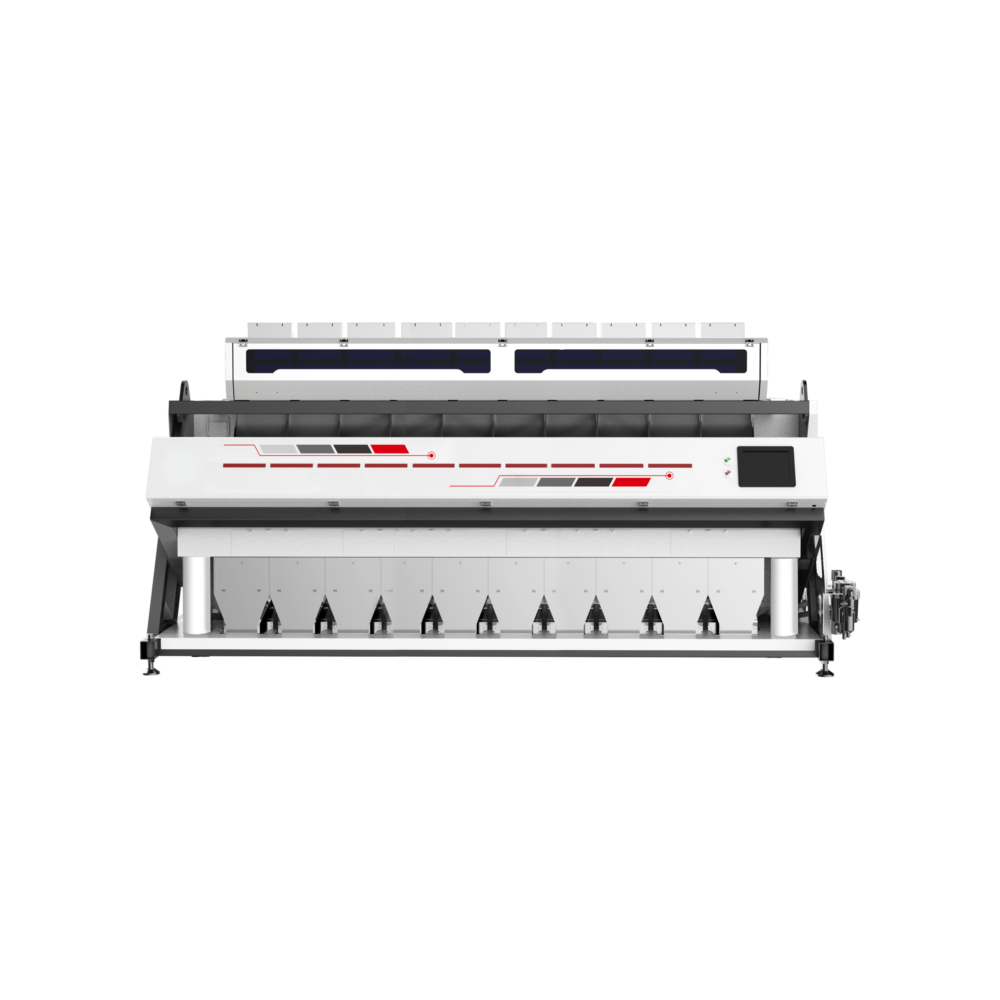
| Parameter | Specification |
| Model | RG10-E |
| Machine Type | Rice Color Sorter Machine |
| Sorting Technology | Optical / Visible-Light Sorting |
| Throughput | 8.5–10 t/h |
| Sorting Accuracy | >99.99% |
| Voltage / Frequency | 220 V / 50 Hz |
| Power | 5.9 kW |
| Weight | 1800 kg |
| Dimensions (L × W × H) | 3293 × 1610 × 1887 mm |
| Typical Sorting Applications | Yellow Rice, Dark Yellow Rice, Chalky Rice, Discolored Rice, Broken Rice |
| Application | Commercial Rice Processing and Quality Sorting |
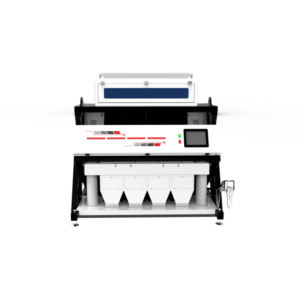
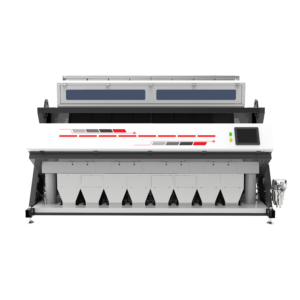
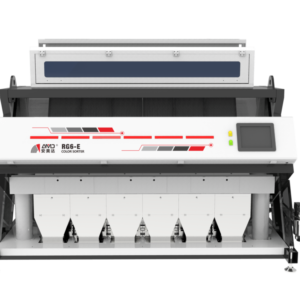
The RG10-E Rice Color Sorter Machine is a high-throughput optical sorting solution designed for large commercial rice mills and processing plants. With a rated processing capacity of 10.2–12 tons per hour, it provides the sorting capacity required for continuous rice production lines where both throughput and finished-product consistency matter.
At higher production volumes, effective rice sorting depends on more than identifying obvious color differences. Material must be distributed consistently, inspected at production speed, classified according to the required quality standard, and rejected at the correct position. The RG10-E combines controlled feeding, optical imaging, intelligent recognition, and targeted rejection to manage these processes continuously.
The system can support sorting tasks involving yellow and dark yellow grains, chalky rice, discoloration, broken grains, visible surface irregularities, and other materials that can be distinguished through optical characteristics. Sorting criteria can be adjusted according to incoming rice conditions and the required finished-product quality.
For processors expanding production or upgrading an existing sorting stage, the RG10-E provides a practical combination of higher throughput, configurable quality control, and stable optical sorting.
As rice processing capacity increases, the optical sorting stage must keep pace with upstream cleaning and milling equipment. If sorting capacity is insufficient, it can become a bottleneck even when the rest of the production line is capable of higher output.
The RG10-E addresses this requirement with a rated throughput of 10.2–12 t/h.
Higher capacity, however, cannot be achieved effectively by simply increasing the amount of rice entering the sorter. A greater material flow must remain sufficiently controlled so that grains can be inspected by the optical system.
The balanced feeding system helps distribute material more uniformly across the sorting channels before it reaches the inspection area. This reduces excessive local concentration and overlapping, creating more stable conditions for image acquisition, recognition, and subsequent rejection.
For processors planning a capacity expansion, the RG10-E is particularly relevant when the existing optical sorting stage is approaching its production limit or when a new rice processing line requires greater sorting capacity from the beginning.
Rice sorting requirements vary according to raw material quality, product grade, processing stage, and finished-rice standards.
Rather than treating one fixed category of rice as universally acceptable or defective, the RG10-E uses optical recognition to classify and separate material according to configured visible characteristics.
Yellow and dark yellow grains can reduce the visual consistency of finished rice.
The optical recognition system identifies visible color differences between the desired product and selected yellow or darkened grains. Once recognized, these grains can be separated according to the configured quality criteria.
Chalky kernels contain visible opaque or chalk-like areas that may fall outside the quality requirements of certain finished-rice products.
The RG10-E can recognize these visible characteristics and support chalky rice separation according to the processor’s selected accept and reject criteria.
The RG-E platform also supports different sorting combinations involving yellow and chalky rice, allowing processors to configure the process according to the desired finished product rather than relying on a single fixed rejection category.
Incoming rice may contain grains whose coloration differs from the desired finished product.
Optical inspection allows these visible differences to be identified and classified according to configured recognition criteria. This helps processors improve appearance consistency across higher-volume production.
For higher-grade finished rice, small surface irregularities can be important even when the overall grain color appears acceptable.
The image-recognition system analyzes characteristics including color, shape, texture, and area. When black spots, peck, localized discoloration, or other surface irregularities create sufficient visible contrast, they can be identified according to the configured sorting standard.
The achievable result depends on the size, contrast, orientation, and visibility of the surface feature during optical inspection.
Not every sorting task involves removing a defective grain. Some rice processing operations require separation according to grain integrity, appearance, or other visible differences.
The RG10-E can support sorting tasks involving broken grains and other visually distinguishable material when the selected characteristics can be reliably recognized by the optical system.
Foreign material can reduce the cleanliness and commercial quality of processed rice.
When impurities differ sufficiently from rice in color, shape, size, texture, or surface appearance, the optical recognition system can support their identification and separation.
Because the RG10-E is an optical visible-light sorting system, separation performance depends on whether the foreign material presents enough visible contrast for reliable recognition. The machine should therefore not be treated as a universal detector for every type of foreign material.
Commercial rice streams often contain several visible variations at the same time.
A processor may need to address yellow grains, chalkiness, discoloration, surface irregularities, broken grains, and visually distinguishable impurities within the same production process.
Configurable recognition criteria allow the RG10-E to adapt the sorting process to actual incoming material and required output quality.
High-volume optical sorting requires image recognition and rejection to remain coordinated as material flow increases.
The RG10-E combines controlled feeding, image acquisition, real-time recognition, material positioning, and rejection to support continuous sorting within its rated production range.
The recognition system evaluates more than a basic light-versus-dark color difference.
Image-processing algorithms analyze visible characteristics including color, shape, texture, and area, allowing the system to distinguish material according to multiple recognition criteria.
This is particularly useful when selected grains or impurities differ from acceptable rice in relatively subtle visual characteristics.
Reliable classification begins with accurate image acquisition.
High-transmittance optical components help reproduce colors and capture subtle visible differences as rice passes through the inspection zone. Clear image information provides the recognition system with a stronger basis for subsequent classification.
At high production volumes, the machine must process image information continuously as material moves through the sorting area.
The sorting system analyzes captured information in real time and applies the configured recognition criteria. Operators can adjust these settings according to changes in incoming rice and required finished-product quality.
Recognition alone is not enough. Once selected material has been identified, the machine must determine its position and coordinate rejection at the appropriate moment.
The positioning system evaluates information related to material trajectory, posture, spatial position, speed, and other movement characteristics. This helps match the recognition result with targeted rejection.
More precise coordination helps remove selected material while reducing unnecessary rejection of acceptable rice.
Uniform material distribution provides the foundation for reliable optical inspection.
The balanced feeding system helps control material flow before rice enters the sorting zone. Reducing excessive concentration and overlapping gives the vision system better conditions for inspecting individual grains.
This becomes particularly important for the RG10-E because its 10.2–12 t/h rated capacity is intended for high-volume processing environments.
The RG10-E is designed for processors whose equipment selection depends on both finished-rice quality and production-line capacity.
The 10.2–12 t/h rated throughput positions the RG10-E for larger rice mills and high-volume processing facilities.
It provides additional sorting capacity when an existing machine restricts production or when a facility plans to increase overall line output.
Optical imaging, multi-feature recognition, controlled feeding, and targeted rejection work together to deliver sorting accuracy above 99.99% under suitable operating conditions.
Actual performance varies according to rice characteristics, incoming material quality, unwanted material concentration, feeding conditions, and required sorting standards.
Rice characteristics can vary between varieties, growing regions, suppliers, storage conditions, and production batches.
Adjustable recognition criteria allow operators to adapt the sorting process to actual incoming material rather than relying on one permanent setting.
Removing more material does not automatically mean better sorting.
Accurate recognition and targeted rejection help limit unnecessary removal of acceptable grains. This supports finished-product quality while protecting usable rice recovery.
The RG10-E is designed to work as part of a commercial rice processing line.
Controlled feeding and continuous optical recognition support stable sorting during extended production runs where both throughput and consistent quality control are important.
A modular machine structure provides convenient access to key sections for routine inspection, cleaning, and servicing, helping simplify day-to-day equipment maintenance.
The RG10-E is particularly suitable for production environments where optical sorting must handle substantial material flow while meeting defined finished-rice standards.
Large rice mills can integrate the RG10-E after major milling and cleaning stages to separate selected visible variations before final grading or packaging.
This allows optical quality control to operate without unnecessarily restricting the output of a higher-capacity production line.
Processors producing higher-grade packaged rice may apply stricter sorting criteria to improve visual uniformity and reduce selected yellow, chalky, discolored, spotted, or otherwise visually inconsistent grains.
Rice intended for export may need to meet specific appearance and cleanliness requirements according to the buyer or target market.
Configurable optical sorting provides an additional quality-control stage for separating selected visible variations and impurities before final packaging.
The RG10-E is also suitable for facilities where upstream production capacity has increased and the existing sorting stage can no longer keep pace.
Matching sorter capacity with the surrounding equipment can help prevent the optical sorting stage from becoming a new production bottleneck.
Some production requirements involve more than one sorting stage or pass.
Depending on incoming material and desired output quality, the RG10-E can form part of a broader rice quality-control process where different sorting stages address different material characteristics.
The RG10-E performs best when its capacity and sorting configuration match the surrounding production equipment.
For an existing facility, processors should determine whether the current sorting stage limits production. For a new line, planned cleaning, milling, grading, conveying, and downstream handling capacity should be considered together.
Important selection factors include:
Evaluating these factors helps determine whether the RG10-E’s 10.2–12 t/h capacity is an appropriate match for the production line and how the sorting criteria should be configured.
The RG10-E has a rated throughput of 10.2–12 tons per hour. Actual capacity can vary according to rice characteristics, incoming material condition, unwanted material concentration, feeding conditions, and required finished-product quality.
The machine supports optical sorting according to visible characteristics. Typical applications include sorting yellow, dark yellow, chalky, discolored, broken, spotted, and other visually distinguishable grains according to configured quality criteria.
The optical recognition system analyzes visible characteristics including color, shape, texture, and area. It can therefore support sorting of selected black spots, peck, localized discoloration, and other visible surface irregularities when they provide sufficient contrast for reliable recognition.
Actual results depend on the visibility and characteristics of the target defect.
The RG10-E can support separation of visually distinguishable foreign material when the impurity differs sufficiently from rice in characteristics such as color, shape, size, texture, or surface appearance.
Because it is a visible-light optical sorting system, it should not be considered a universal detection solution for foreign materials that are visually indistinguishable from the surrounding rice.
Yes. Operators can configure recognition criteria according to different visible characteristics and combined sorting requirements based on incoming material and desired finished-product quality.
Yes. The RG10-E can be considered when an existing sorting stage limits production capacity or when a rice mill plans to increase hourly output.
The capacity of upstream and downstream equipment should also be evaluated before selection to ensure that the sorter fits the complete production line.
The main documented difference relevant to capacity selection is throughput. The RG8-E is rated at 8.5–10 t/h, while the RG10-E is rated at 10.2–12 t/h.
If a processing line normally operates below 10 t/h, selecting the larger model solely for its maximum capacity may not provide a practical advantage. Model selection should match actual line throughput and sorting requirements.
Sorting performance depends on the relationship between material flow, incoming rice condition, target concentration, feeding stability, and required output quality.
Operators should configure feeding and sorting parameters according to actual production requirements rather than simply maximizing material flow.
Consider current production capacity, planned expansion, rice variety, incoming material condition, primary sorting targets, visible impurity levels, required finished-product quality, and surrounding equipment capacity.
For applications with specific sorting requirements, representative sample evaluation can help determine an appropriate configuration.
The RG10-E Rice Color Sorter Machine is designed for commercial rice processors that need greater optical sorting capacity within a continuous production line.
With a rated 10.2–12 t/h throughput, multi-feature image recognition, balanced material feeding, configurable sorting criteria, and targeted rejection, the RG10-E provides a practical solution for improving finished-rice consistency while supporting higher production volumes.
The appropriate configuration depends on actual processing conditions rather than throughput alone. Rice variety, incoming material quality, visible defects and impurities, required finished-product standard, and existing production-line capacity all influence equipment selection.
Planning a new high-capacity rice processing line or upgrading your current sorting stage?
Send PolySorter your rice type, sample photos, current line capacity, target throughput, main defects or impurities, and required finished-product quality. Our team can evaluate the application and recommend an appropriate sorting configuration.
Contact PolySorter to discuss your RG10-E rice sorting project and request a quotation.